Session 3: 3D Printing

Session 3
3D Printing
A Router Can Only Take Material Away
Every part in Session 2 started as a sheet, and the router cut away whatever wasn't the part.
That can't make a clip with a hook, a mount with a pocket for a wire, or anything hollow. A printer starts with nothing and adds.
It Builds One Layer at a Time
FDM (fused deposition modeling): plastic filament is melted in a hot nozzle and laid down as a thin bead.
It Builds One Layer at a Time
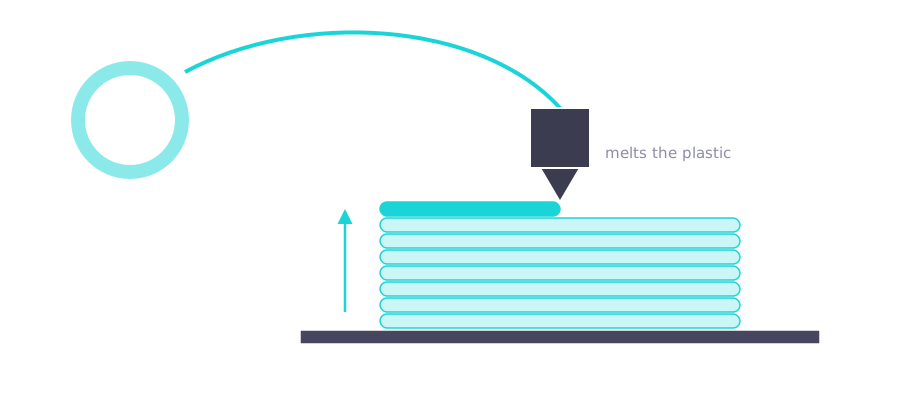
Before it prints, a slicer cuts your model into hundreds of flat layers and plans the nozzle's path through each one.
Every Print Has a Weak Direction
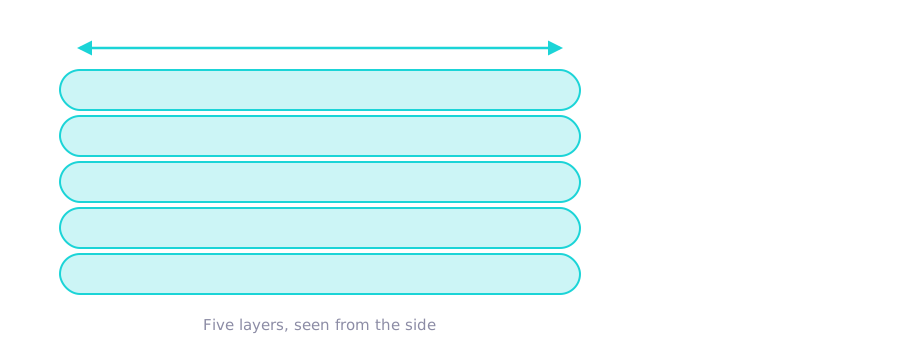
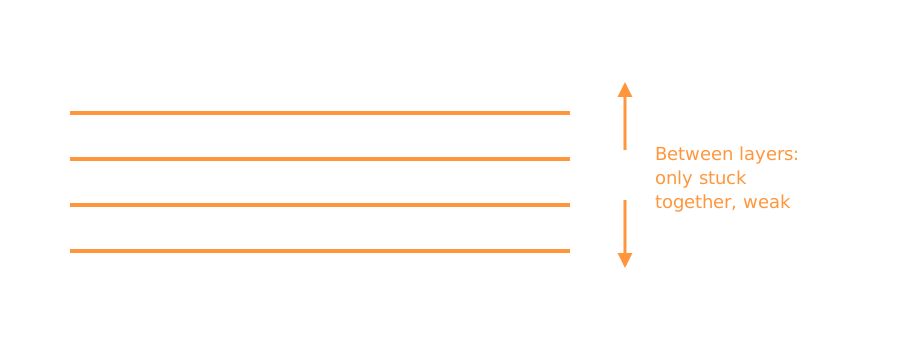
Each new layer is only fused to the one under it. Pull along the layers and you're stretching plastic; pull across them and you're peeling them apart.
Same Bracket, Two Ways
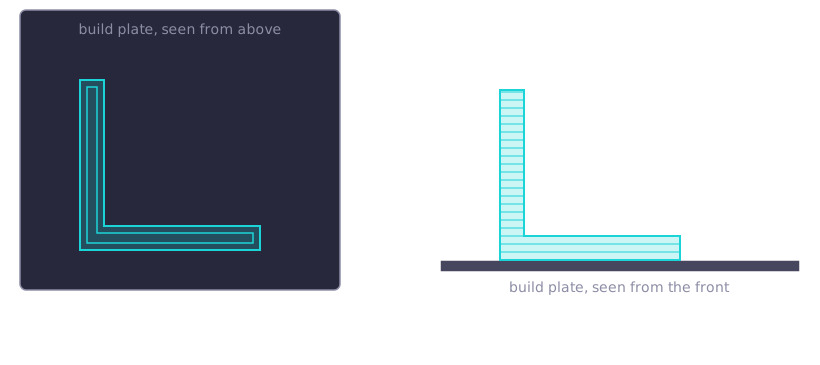
Same file, same plastic, same settings. Pull both arms sideways. Which one snaps first?
Same Bracket, Two Ways
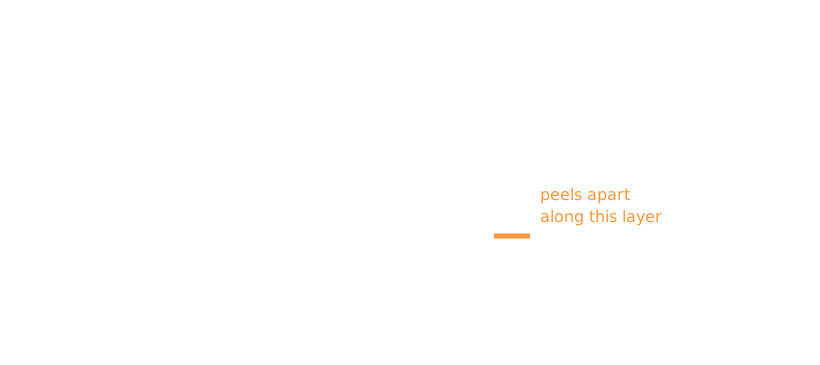
B's arm is a stack of layers, and the pull peels off the bottom one. You'll print both today and measure how much weaker in Session 5.
Most of a Print Is Air
Infill: the pattern printed inside the walls. 20% infill is 80% air.
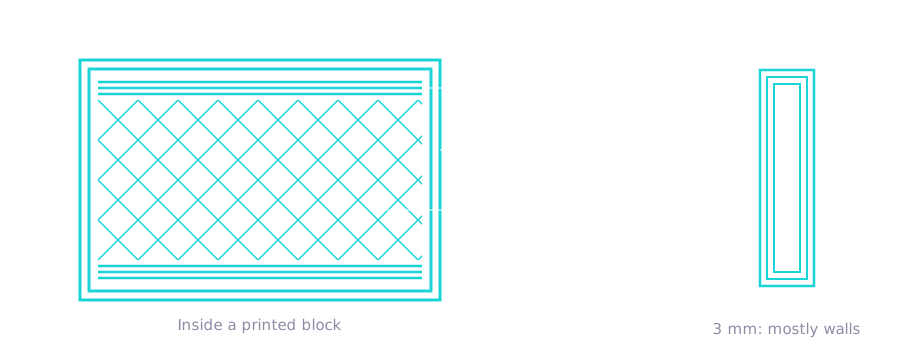
Your bracket's 3 mm arm is nearly all wall. More infill changes the middle, not the bond between layers.
Plastic Can't Print Onto Air
Every layer has to sit on the one below it. Lean past about 45° and the layer starts printing onto nothing.
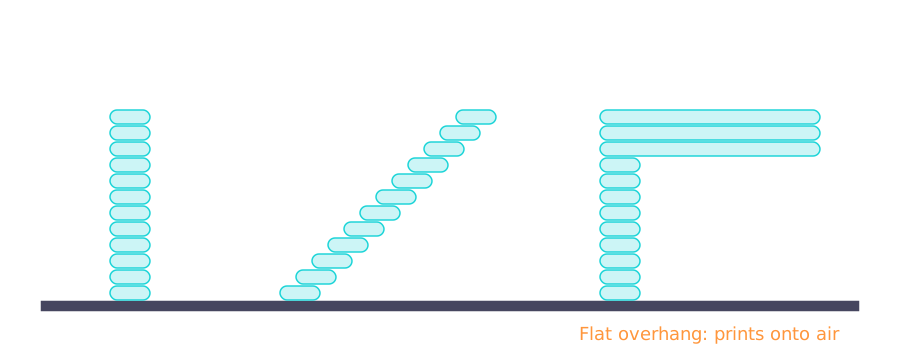
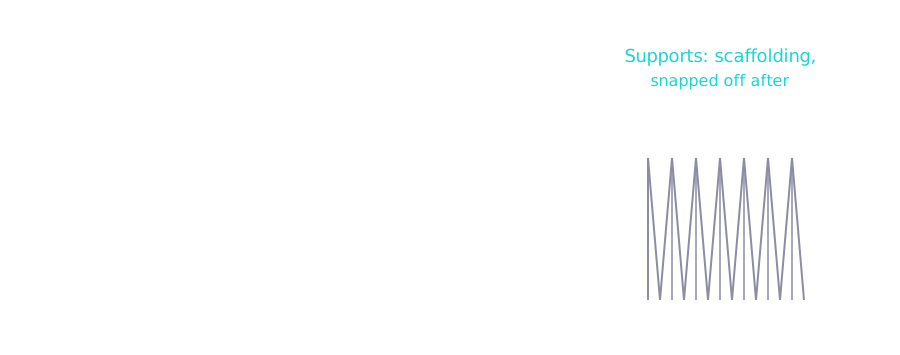
Supports: throwaway scaffolding the slicer adds under an overhang, snapped off after.
Thin Layers Cost Time
Layer height: how thick each layer is. The 3D45 prints from 0.05 mm to about 0.3 mm.
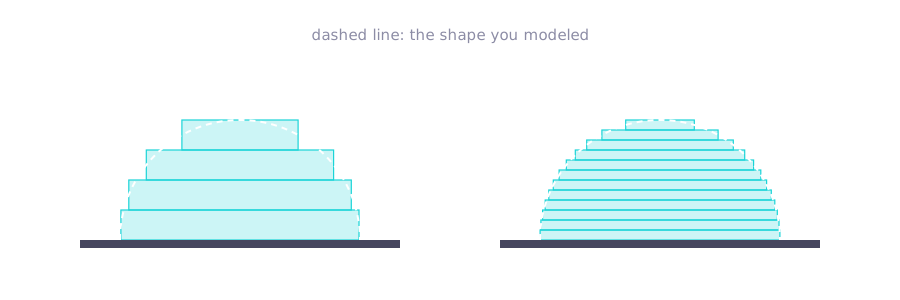
Today's brackets use 0.2 mm. Nobody needs a smooth bracket they're about to break.
PLA Is Easy. PETG Takes the Heat.
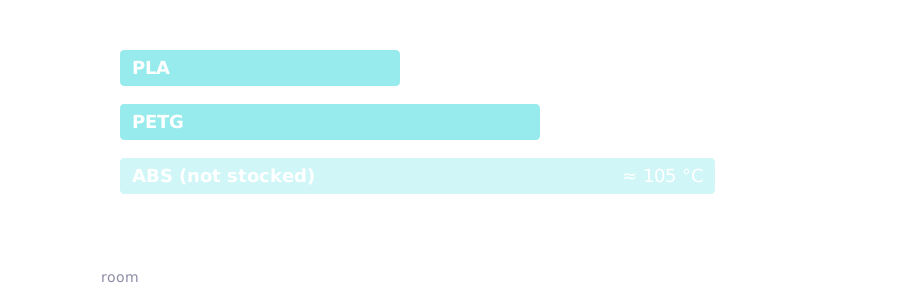
PLA prints easily and holds its shape, but it's brittle and softens around 60 °C. PETG is tougher, bends before it breaks, and takes more heat, but it strings more.
A part that lives somewhere warm is a PETG part.
The 3D45 Reads the Spool
Dremel spools carry a tag the printer reads, so it sets its own nozzle and bed temperatures. You choose the shape, the orientation, and the settings.
Its build volume is 254 × 152 × 170 mm. Bigger than that, and it's a router part.
Route It or Print It?
Three questions settle most parts:
- Is it big and flat, or small and oddly shaped?
- Does it carry real load, or just hold its own shape?
- Do you need many, fast and cheap, or one custom part worth hours of print time?
Route It or Print It?
A side panel is big, flat, and structural: the router. A custom joystick bezel is small and oddly shaped: the printer.
The cabinet needs both. Printing is a real option for the right part, not a way around the router.
Start It Before You Leave
Model the bracket, put both orientations on one plate, write your prediction, and start the print. It runs overnight.
Next Time
Session 4: CNC Safety Certification, on both routers.
Session 5 opens by breaking today's brackets.
'F' → Fullscreen
Build
Each group has one printer and prints one plate: two copies of the same bracket, one on its side and one standing up. Steps 1–5 are today; Step 6 is the start of Session 5.
Step 1: Model the Bracket
In OnShape, model this L-bracket to the exact dimensions. Sketch the L, extrude it 12 mm, then cut the Ø5 hole through the upright arm: that's where the spring scale hooks on in Session 5.
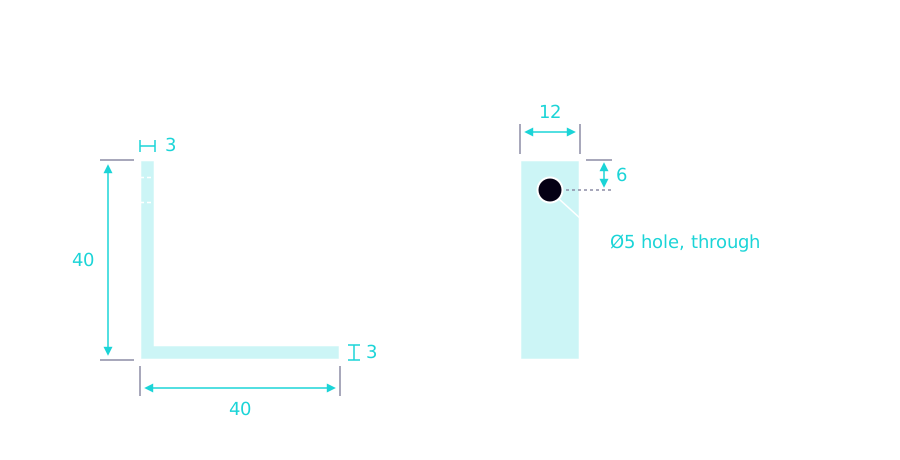
Export it as an STL (right-click the part, then Export), named s3-bracket- plus your group name.
Step 2: Two Copies, One Plate
- In Dremel Print Cloud, click + Upload new, then Choose file, pick your STL, and click Save and go to My Files.
- On your file's row, click Layout.
- Extra → Copy adds the second copy. Each copy gets its own row on the left.
- To turn a copy, click its row, choose Rotate, and use the −90 and +90 buttons. Then click On bed so it sits on the plate.
- Copy A, on its side: the L shape lies flat on the plate. Your STL probably arrives this way.
- Copy B, standing up: the long arm flat on the plate, the other arm pointing straight up. From copy A, that's +90 on X.
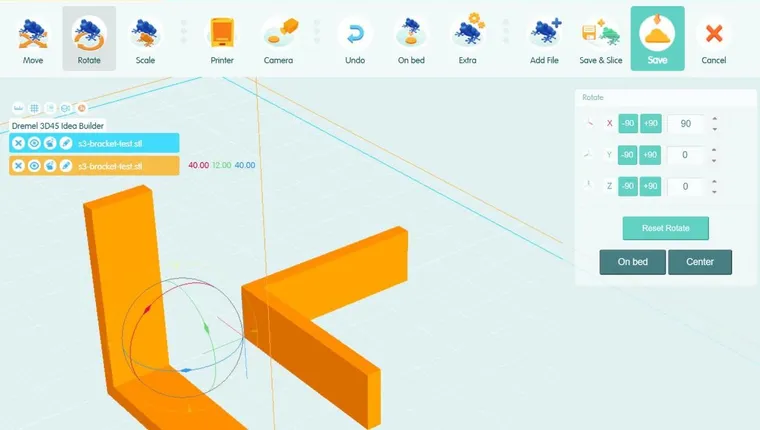
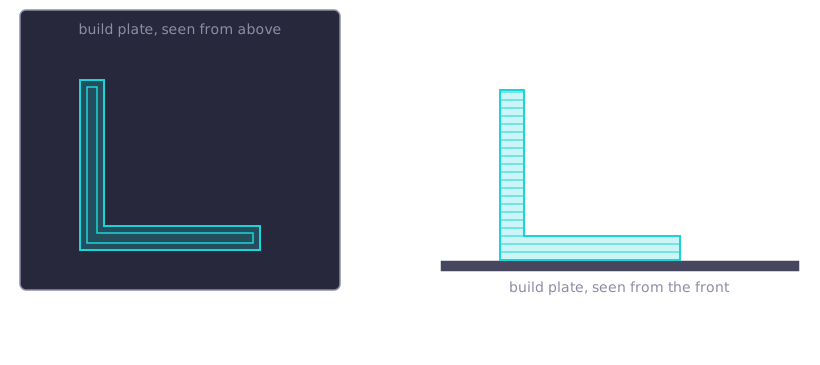
Click Save & Slice. On the settings screen, choose the profile Standard (PLA), which sets a 0.2 mm layer height. Then change two things it gets wrong for this test: Infill Density to 20 (it starts at 50), and untick Supports (it starts on).
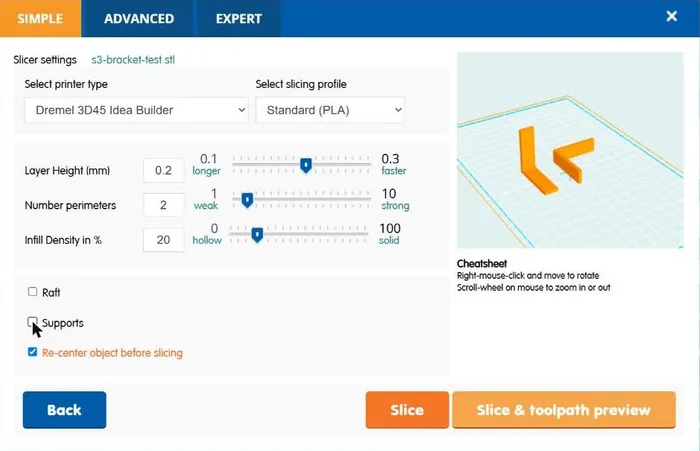
Both copies are on the same plate, so the plastic, the settings, and the printer are identical: orientation is the only thing that's different.
Step 3: Find the Overhang
Click Back to return to the layout. Add a third copy and stand it on the end of its upright arm, so the other arm sticks out sideways at the top. Then Save & Slice again, tick Supports, and click Slice & toolpath preview.
Write down what the slicer added, and where. Then delete the third copy and turn supports back off. It's not part of the print.
Step 4: Predict, Then Print
Before you start the print, write down which copy you think will snap at the lower force, and roughly how many times stronger you think the other one is.
With the settings from Step 2, click Slice & toolpath preview. The preview's Info box shows the Estimated print time; record it. Then send the job to your group's printer. Stay until the first layer goes down cleanly: a bad first layer is the most common failed print.
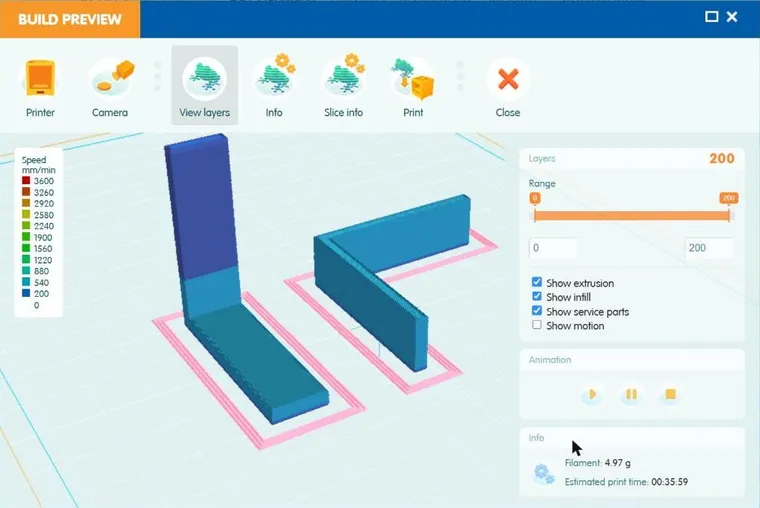
Step 5: Route It or Print It?
While it prints, decide for each arcade cabinet part: routed from sheet stock, or 3D printed? Justify each with at least one of the three questions, not a guess.
- Side panel
- Joystick and button mounting bezel
- Marquee light mount bracket
- Control panel base
- Cable management clip
Step 6: The Break Test (Start of Session 5)
Safety glasses on. PLA snaps, and pieces fly.
- Clamp the long arm flat in a vise, with the upright arm pointing up.
- Hook the spring scale through the hole.
- Pull slowly, straight sideways, at a right angle to the arm's flat face. A teammate watches the scale and calls out the reading at the moment it breaks.
- Repeat with the other copy.
If a bracket bends past the end of the scale without breaking, record it as more than the scale's maximum: that's still a result. Then look closely at each break surface and describe it.
Reference: The Three Filaments
| PLA | PETG | ABS | |
|---|---|---|---|
| In our shop | Yes | Yes | No |
| Ease of printing | Easiest | Moderate: strings more | Hardest |
| Strength and toughness | Rigid, brittle | Tougher, bends before breaking | Strong, impact-resistant |
| Softens around | 60 °C | 80 °C | 105 °C |
| Warping risk | Low | Low to moderate | High: needs an enclosure |
Checkpoint
- Is orientation the only difference between copies A and B?
- Same file, same plate, same settings. If anything else differs, the break test can't tell you what caused the result.
- Did your prediction go on paper before the print started?
- A prediction written after the break is just a description.
- Did every route-or-print decision name a reason?
- Point to size and shape, load, or how many you need. "Printing is cool" isn't one.
Reflection
Answer these on your own, after the break test. Reflections are individual, even when the rest of the session was team work.
- Which copy broke at the lower force? Describe its break surface, and use it to explain why it broke there.
- Name one arcade cabinet part your team might print. Which way would you put it on the plate, and why?
- Is there a part in Step 5 you're genuinely unsure whether to route or print? What specific information would settle it?
Submit
After the break test in Session 5, submit your sheet with both break results, your route-or-print decisions, and your reflection.