Session 5: CAD Assemblies

Session 5
CAD Assemblies
That Bracket Was One Part
You just broke a single printed part. A cabinet is a dozen parts, and every one of them meets another one at a corner.
Freshman year you modeled one part at a time. Today you make several parts meet, at the right size, with nothing left to luck.
Parts Live in One Place, Fit in Another
- A Part Studio is where you model the parts: each panel, its size, its thickness.
- An Assembly is where you bring finished parts in and tell them how they sit against each other.
A Mate Is a Rule, Not a Position
Dragging a panel until it looks right puts it somewhere. A mate tells OnShape where it belongs, and keeps it there when anything else changes.
A Mate Is a Rule, Not a Position
The one you'll use for a cabinet is Fastened: it locks two parts together as if they were screwed, which is exactly what a cabinet joint is.
Drag a panel that's only been positioned by eye and it slides away. Drag a fastened one and the whole box comes with it.
You're Given the Outside. Nothing Else.
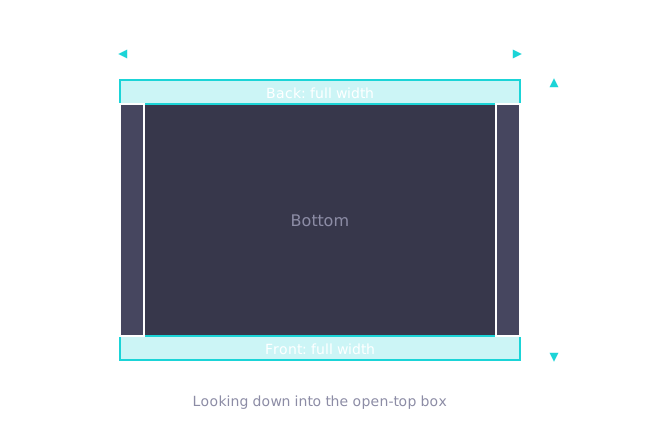
A client asks for a box 160 × 120 mm on the outside. The front and back run the full 160. The sides fit between them. So how long is a side panel?
You're Given the Outside. Nothing Else.
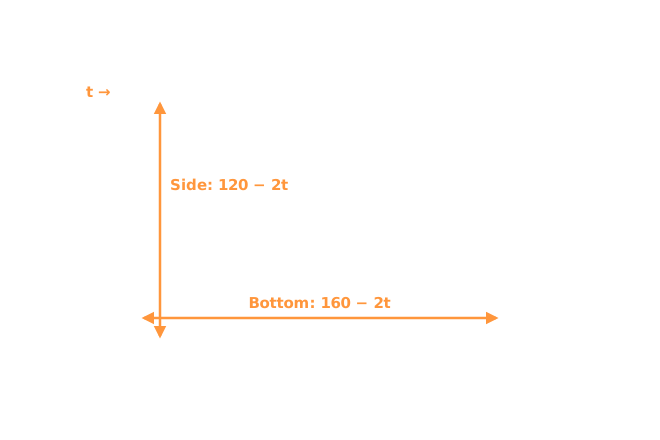
Not 120. The front and back each take up one thickness of that 120, so a side is 120 − 2t. The bottom sits between the sides too: 160 − 2t wide.
Predict It
The sheet measures 5.80 mm thick. How long is a side panel, and how wide is the bottom?
Side: 120 − 2 × 5.80 = 108.40 mm. Bottom: 160 − 2 × 5.80 = 148.40 mm.
Cut the side at 120 instead and the box comes out 131.6 mm deep. The client asked for 120.
Model What You Measure, Not the Label
Sheet goods are almost never their label. "6 mm" plywood is often 5.6 or 5.8, and "12 mm" is often 11.7.
Model the label and every derived panel inherits the error, twice. That's why the calipers from Unit 1 Session 6 come out today.
Type the Thickness Once
OnShape lets you store a number as a Variable named t. Then every size you type can use it: 120 mm - 2*#t, not 108.4.
The mm matters. #t is a length, and OnShape won't subtract a length from a plain number: leave the unit off and the dimension turns red.
When a new batch of plywood measures differently, you change one number and every panel resizes itself. Type 108.4 by hand and you'll have to find it and fix it yourself, and the one you miss will show up as a gap.
Model Each Panel Flat
Sketch each panel lying flat and extrude it #t up. That's how it will sit on the router bed.
A panel has two jobs. Its thickness makes the joints fit in the assembly. Its shape is what CAM will turn into a cutting path in Session 8.
"Part 1" Will Hurt You Later
Five panels named Part 1 through Part 5 are fine for about ten minutes. In the assembly, and again in CAM, you'll be picking them out of a list.
Name every part as you make it: Front, Back, Left Side, Right Side, Bottom.
Two Things to Remember
A clean-looking box can still hide a bad joint.
Zoom into every corner on its own, and measure the outside. A glance at the whole box proves nothing.
Two Things to Remember
The test of a good model is changing it.
Today ends with a new thickness. If your box still measures 160 × 120 × 100 with every corner closed, it was built right. If not, it shows you exactly which panel wasn't.
Today
- Break the Session 3 brackets
- Measure the stock and store it as
t - Model five panels from the outside size, and fasten them into a box
- Change
tand see whether your box survives
Next Time
Session 6: CAD Assembly Practical
A different box, on your own, graded on the OnShape document. Everything you do today is on it.
'F' → Fullscreen
Build
Step 1: Break the Brackets
Do Session 3's Step 6 with your group: both brackets, the spring scale, safety glasses on. Record both forces and both break surfaces on your Session 3 sheet and hand it in. Then everyone works alone in OnShape.
Step 2: Measure the Stock
With calipers, measure the thickness of the sheet your instructor hands out at three places, at least 20 mm in from the edge. Record all three and their average, to two decimal places. If there's no sheet at your table, use the value your instructor gives you.
Step 3: Store It as a Variable
- Create a new OnShape document named Session 5 Box - your name.
- Switch it to millimeters first. New documents start in inches: ≡ menu → Workspace units… → Length default unit: Millimeter, then the check mark.
- In the Part Studio, open Search tools in the toolbar, type variable, and choose Variable.
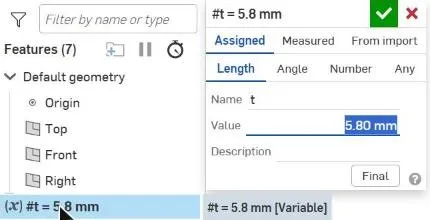
- Leave it on Length. Name it
t, type your average, and click the check mark. It appears in the feature list as #t.
Step 4: Model Five Flat Panels
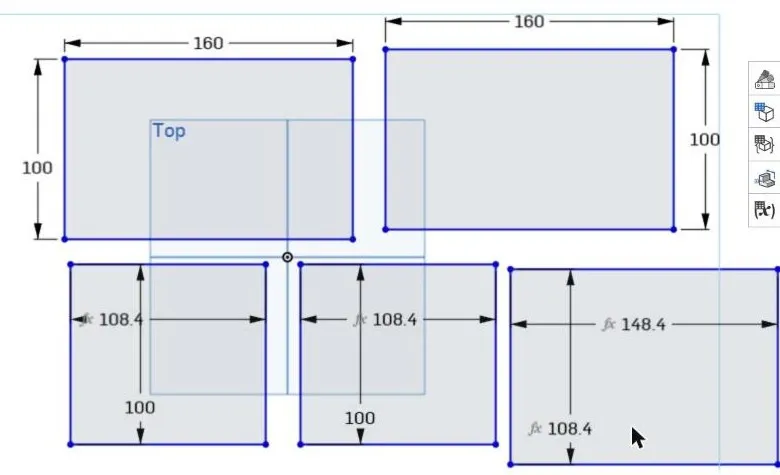
The box is 160 mm wide, 120 mm deep, and 100 mm tall on the outside, with an open top. The front and back run the full width, the sides fit between them, and the bottom fits inside all four walls.
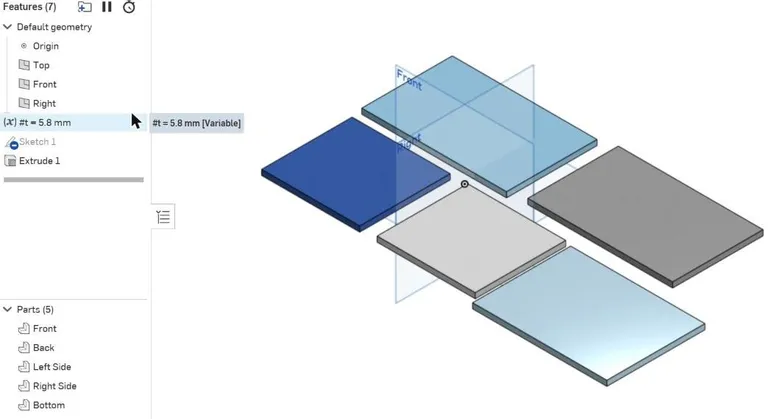
- Sketch the five panels as rectangles on the Top plane, apart from each other. One sketch with all five is fine.
- Dimension each one. Type every size that depends on thickness as an expression with its unit, for example
120 mm - 2*#t. Never type the result. Click the green check to accept it; pressing Enter can pick OnShape's#tsuggestion instead. - Extrude all five at once, New, with the depth set to
#t. Each rectangle becomes its own part. - Rename each part as you make it: Front, Back, Left Side, Right Side, Bottom.
Before you model, fill in the panel sizes on your sheet, as expressions and as numbers for your t. Every size that came from an expression shows ƒx in front of it.
Step 5: Fasten Them Into a Box
- Open the Assembly tab, click Insert, and click Part Studio 1. All five parts come in at once.
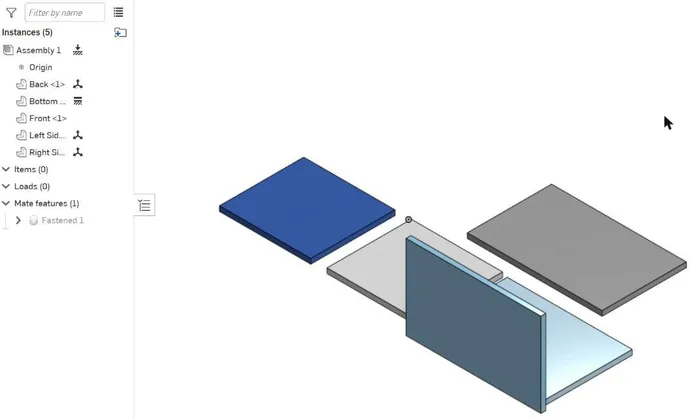
- Right-click the Bottom and choose Fix, so it stays put. The small icon beside each other part means has degrees of freedom: nothing holds it yet.
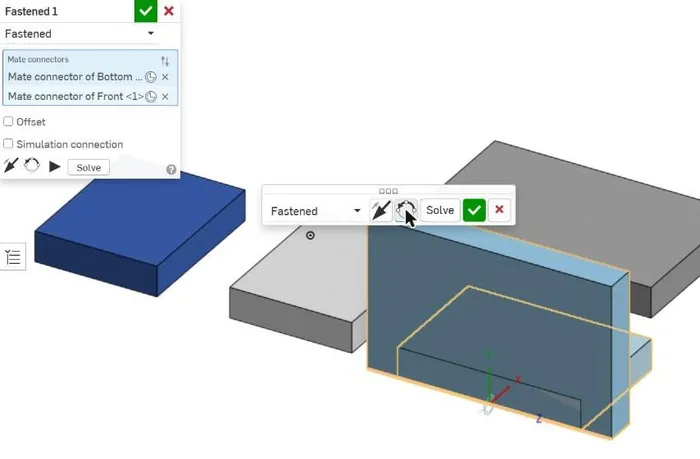
- Fasten each wall to the bottom, one at a time. The bottom sits inside the four walls, flush with their lower edges, as in the diagram. Open Fastened mate, then:
- On the bottom, click the midpoint of the lower edge where this wall goes. It lights up orange.
- On the wall, click the midpoint of the long edge that will sit at the bottom of the box.
- The wall jumps over, probably lying flat. Click Reorient secondary axis (the circular arrows) until it stands up. It turns a quarter-turn per click.
- Click the Top face of the view cube and look down. The wall must sit outside the bottom, not on top of it. If they overlap, click Flip primary axis, then reorient until it stands up again.
- Click the green check. The wall's degrees-of-freedom icon disappears.
Step 6: Check It
- With the Measure tool, measure the outside width, depth, and height. It should read 160 × 120 × 100.
- Zoom into each of the four vertical corners, one at a time: no gap, no overlap.
- Drag one wall. If it moves on its own, it was never fastened.
Step 7: Change the Thickness
Your instructor gives everyone a second thickness, a different batch of plywood. In the Part Studio, edit your t Variable to that value. Then go back to the Assembly and check it again, exactly as in Step 6.
A correct model still measures 160 × 120 × 100 with every corner closed. If something moved, find the panel responsible: it has a typed number where it needed #t. Fix it, and write down what you fixed.
Checkpoint
Before you move on, confirm:
- Your
tVariable holds a measured thickness, to two decimal places, not a label value - All five parts are named, and every thickness-dependent size uses
#t - The assembly measures 160 × 120 × 100 at both thicknesses, with all four corners closed
- Every wall is held by a real Fastened mate, not placed by eye
Reflection
Answer these on your own. Reflections are individual, even when the rest of the session was team work.
- When you changed
t, which panel sizes changed and which stayed exactly the same? Explain why, using the words "between" and "full width." - What's the difference between a panel's thickness mattering and a panel's shape mattering — and where does each one actually get used?
Submit
Submit your Session 3 sheet with the break results, your OnShape document's link, your sheet with the panel sizes and anything you fixed in Step 7, and your reflection.